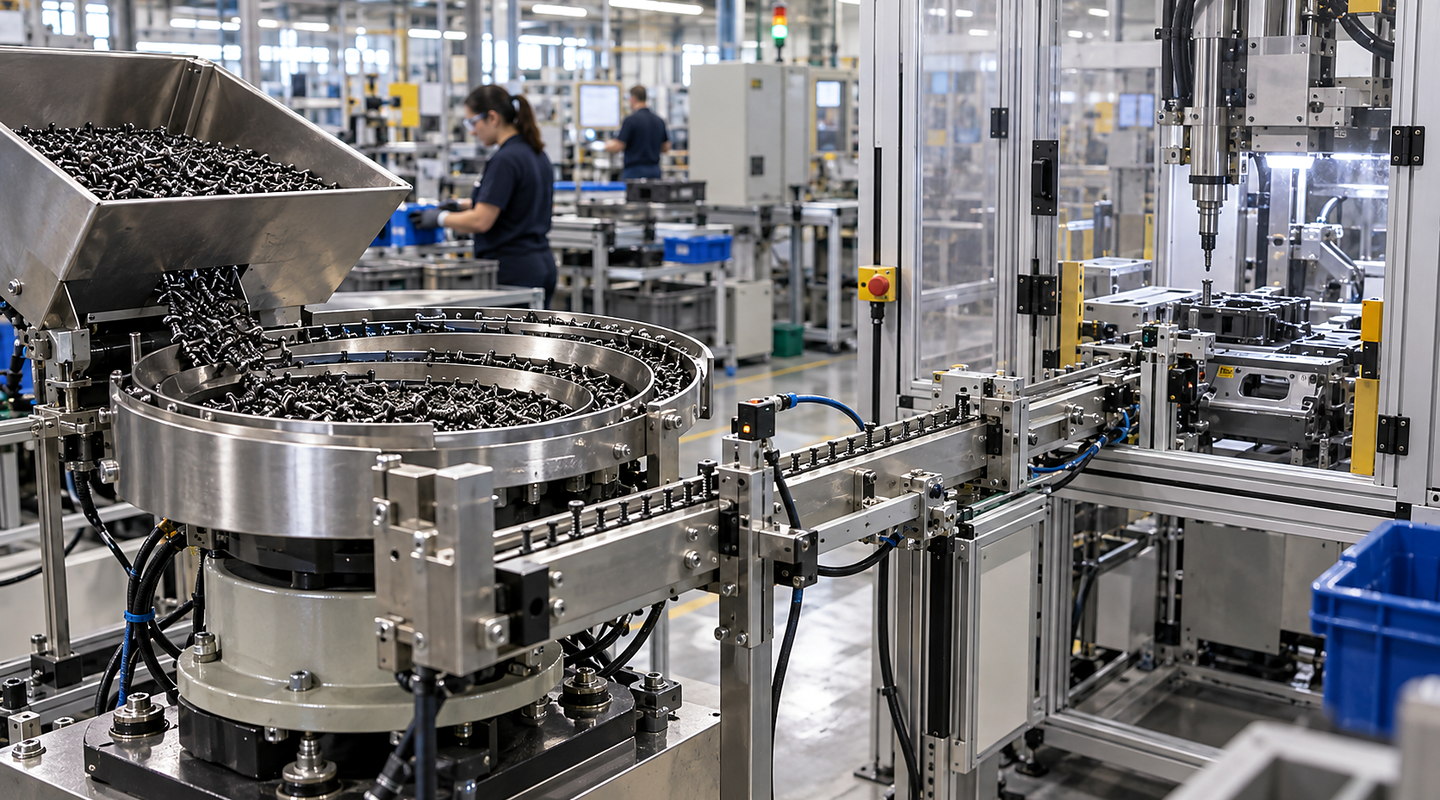
Threaded Insert Feeders FAQs
Straight answers to common questions about threaded insert feeders, including suitable applications, limitations and what to send us.
Useful answers about threaded insert feeders depend on your application, operating range and the results you need.
Your final threaded insert feeders scope must also account for escapement and downstream pick interface, jam, damage and recovery acceptance checks, current regulations and the conditions at your site.
Get practical answers for your application — Threaded Insert Feeders
Plan threaded insert feeders around real component variation, bulk condition, orientation, usable delivery rate and the downstream interface. Discuss representative part trials with Sorting Solutions. The answers below explain suitable applications for Threaded Insert Feeders, what information helps and what still needs an application-specific check.
Discuss your application
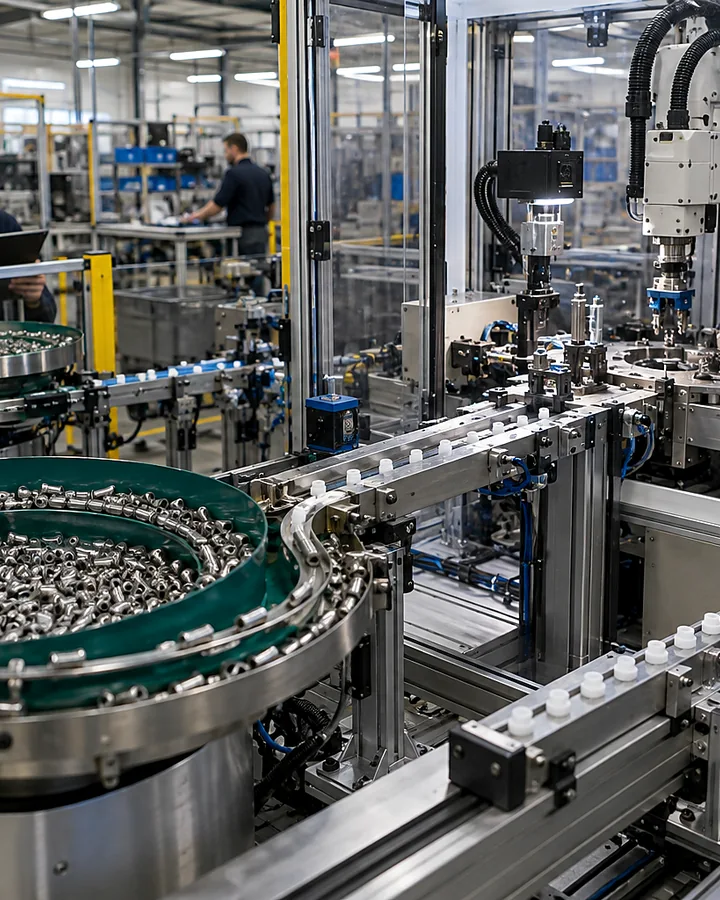
Practical answers about threaded insert feeders
How do we present threaded inserts to an insertion machine?
For threaded insert feeders, test representative production components for separation, orientation, damage risk and usable delivery rate. Choose the feeding principle by real part behaviour, surface, fragility and entanglement behaviour and jam, damage and recovery acceptance checks, not nominal feeder speed alone.
How should a project for threaded insert feeders begin?
Start with labelled insert samples and drawings, the required leading end and the receiving tool sequence. Identify protected surfaces and credible nesting or paired-part behaviour. The geometry and variation guide helps separate confirmed facts from conditions that need a trial.
Can you quote threaded insert feeders from a short description?
An early budget range may be possible, but a reliable scope for bulk presentation using threaded-insert feeding for assembly needs the product or part range, line connections, site conditions and your requirements for jam, damage and recovery acceptance checks.
What information should we send about threaded insert feeders?
Send the approved insert references, normal supply condition, permitted contact areas and receiving-tool details. Include demand and occupied states, changeover practice, available space and services, and any records of damage or interrupted delivery. State what remains uncertain.
How will performance be checked?
Measure correctly presented inserts accepted by the downstream process over an agreed operating pattern. Include replenishment, variant changes and assessed recovery cases; report jams, damage and unaccepted delivery separately. A feeder running or a presence signal alone does not prove the required insert reached the tool.
What are the main limitations?
Sample trials must include normal, marginal and supplier-variant components. Quoted feeder output is not the same as usable delivery at the downstream process. Fragile, flexible, magnetic or entangling parts may need a different presentation method.
What alternatives should be considered for bulk presentation using threaded-insert feeding for assembly?
Compare flexible vision-guided feeding for suitable variable part families with manual or tray presentation where bulk feeding would damage parts or add unjustified complexity. For Threaded Insert Feeders, the practical option may be simpler than the most automated one.
Can the proposed solution guarantee regulatory compliance?
No solution can guarantee compliance on its own. Applicable law, current standards, risk assessment, validation and conformity responsibilities must be addressed for your complete application.
Who will handle my enquiry?
Sorting Solutions will receive enquiries from threadedinsertfeeders.co.uk. Call 01844 617223 or email sales@sortationsolutions.co.uk to speak with the team directly.