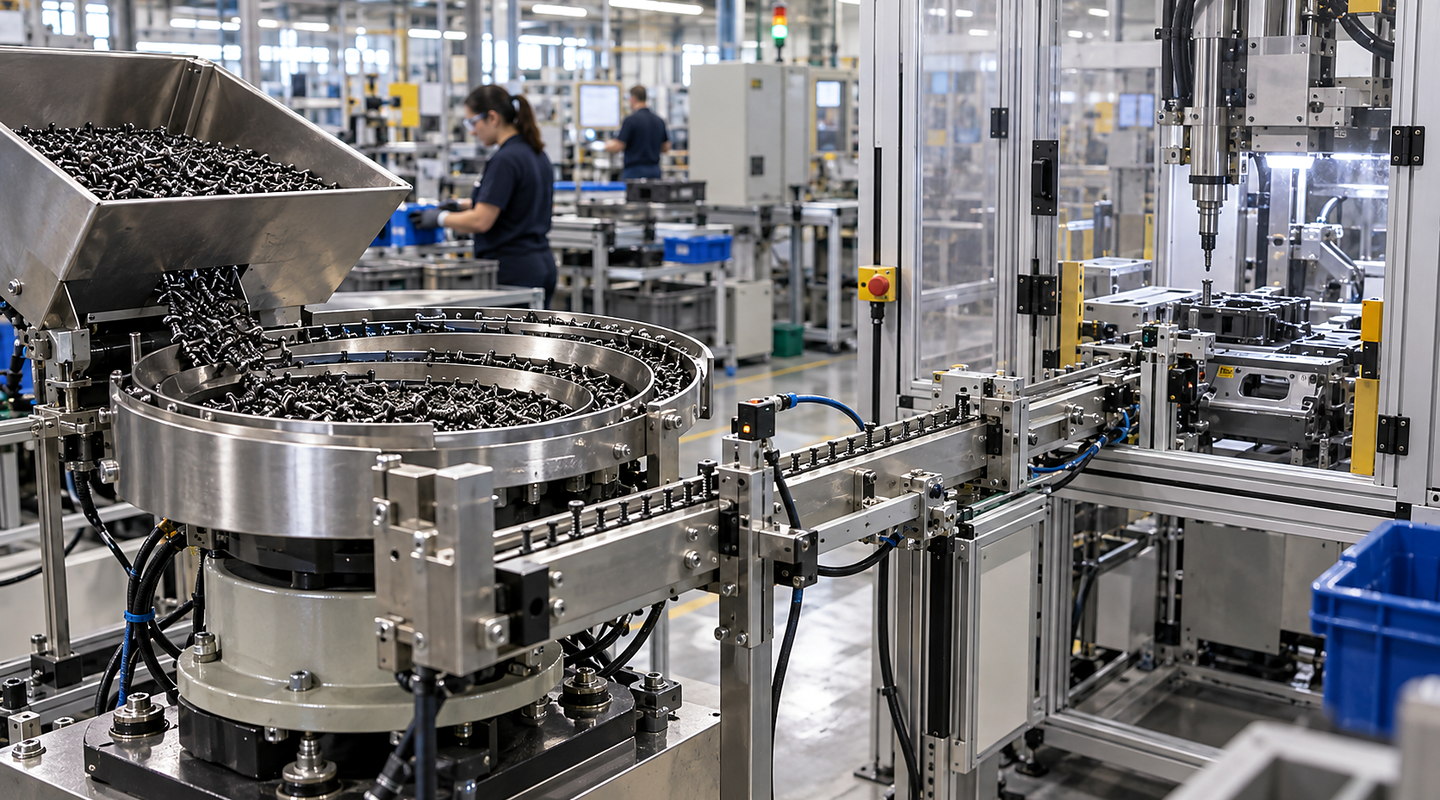
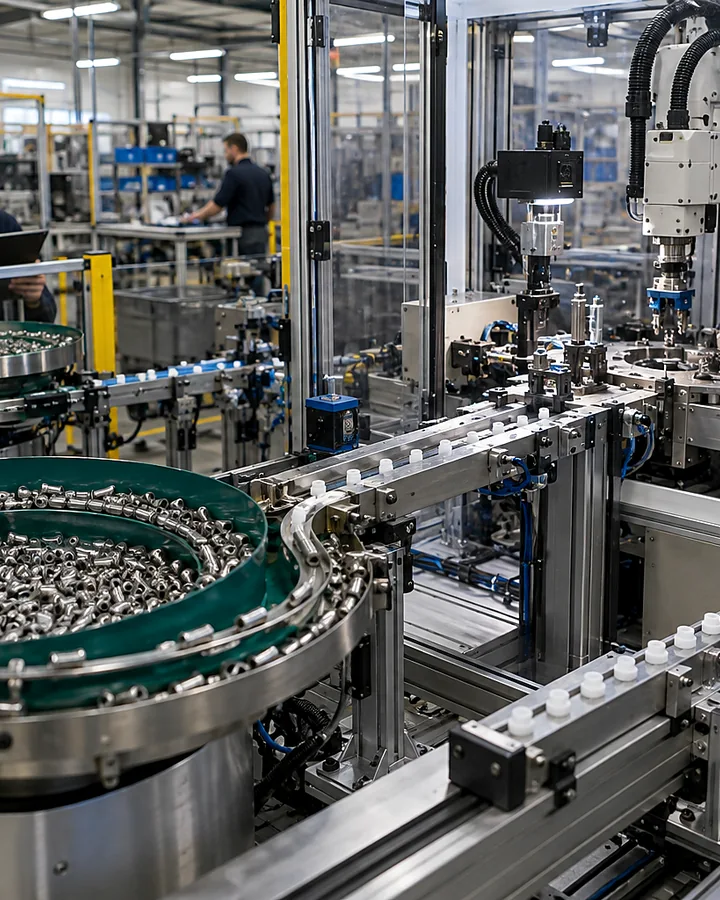
Bulk Presentation Using Threaded-Insert Feeding for Assembly
Plan bulk presentation using threaded-insert feeding for assembly around representative components, bulk condition and the downstream interface, line connections, operating limits, acceptance checks and next steps.
In brief
Bulk presentation must turn loose inserts into individual parts in the pose the receiving tool requires. Define the insert family, leading end and permitted contact surfaces, then trial separation and release with ordinary bulk supply. Assess parts accepted at the tool, not movement around the feeder alone; start with the insert geometry and variation guide.
Plan threaded insert feeders around real component variation, bulk condition, orientation, usable delivery rate and the downstream interface. Discuss representative part trials with Sorting Solutions.
On the production floor
Plan for the conditions your team handles every day — Threaded Insert Feeders
Plan threaded insert feeders around real component variation, bulk condition, orientation, usable delivery rate and the downstream interface. Discuss representative part trials with Sorting Solutions. For bulk presentation using threaded-insert feeding for assembly, the deciding details include component geometry and variation for threaded-insert feeding for assembly, bulk condition and replenishment method and jam, damage and recovery acceptance checks.
Details worth resolving early for bulk presentation using threaded-insert feeding for assembly
Question 1
Component Geometry and Variation for Threaded-Insert Feeding for Assembly
Provide labelled samples and drawings for each length, thread and external profile. Mark the flange, slot, knurl or end feature used to distinguish orientation, and identify similar variants that must not be mixed.
Question 2
Surface, Fragility and Entanglement Behaviour
Mark threads and other functional surfaces that must remain undamaged, together with permitted tooling contact. Include normal finish and residues; examine inserts after circulation and transfer as well as after a single pass.
Question 3
Bulk Condition and Replenishment Method
Describe the delivered bulk condition, working fill range and replenishment method. Observe nesting, bridging or parts travelling together where credible for the insert family; a hand-arranged sample does not represent loose supply.
Question 4
Required Orientation and Delivery Rate
Show the required leading end at discharge and at the receiving tool, including rotational position if it matters. Define the operating pattern and count correctly presented inserts accepted by the downstream process over the agreed trial period.
Question 5
Escapement and Downstream Pick Interface
Define the release position, support during transfer and the point at which the tool takes control. Agree how the feeder and receiver distinguish demand, readiness and an occupied position before another insert is released.
Question 6
Jam, Damage and Recovery Acceptance Checks
Agree records for jams, damaged inserts, suspected pairs, wrong orientation and interrupted insertion. State the assessed response and restart checks for each relevant condition; do not assume a part-present signal identifies the insert specification.
Your operating cycle
Plan for more than automatic running
Include replenishment, normal production, planned change, short stops, fault recovery, cleaning and maintenance for bulk presentation using threaded-insert feeding for assembly. A fast automatic step can still leave your team with a slow or awkward overall process.
Normal production and variant changes
Replenishment and material presentation
Operator access and safe interventions
Cleaning, maintenance and recovery
Prove the result
Test bulk presentation using threaded-insert feeding for assembly against representative components and difficult bulk-presentation conditions
Normal production
Run the agreed product or part mix for bulk presentation using threaded-insert feeding for assembly at your intended operating pattern.
Difficult conditions
Include credible extremes for component geometry and variation for threaded-insert feeding for assembly and surface, fragility and entanglement behaviour.
Fault and recovery
For each agreed exception, record what was observed, how the affected insert was accounted for and the first accepted delivery after recovery. Use the assessed trial and intervention method; do not force a jam or bypass a safeguard to create a test result.
Important limits
Be clear about what the trial has shown
Sample trials must include normal, marginal and supplier-variant components.
Quoted feeder output is not the same as usable delivery at the downstream process.
Fragile, flexible, magnetic or entangling parts may need a different presentation method.